Packaging inspection systems UK
Catch packaging defects before they leave your line
Machine-vision inspection and automatic reject systems for bottles, cans, jars, pouches, blisters, labels, date codes, barcodes, fill levels, cases and pallets—engineered around your production process.
Packaging inspection systems
Packaging formats and critical quality checks
Every material, surface and defect behaves differently under a camera. We design the optics, handling and controls as one system—then prove the checks with real samples.
Vision inspection systems
Combine industrial cameras, controlled lighting, decision software, PLC interfaces and automatic reject control.
Explore the systemBottle inspection
Check bottle condition, fill level, closures, labels and codes at production speed.
Explore the inspectionJar inspection
Verify jar condition, contents, lid application, labels and traceability marks.
Explore the inspectionPouch inspection
Inspect seals, print, codes, orientation and pouch presentation before despatch.
Explore the inspectionCarton inspection
Check carton closure, print, labels, codes, orientation and visible pack damage.
Explore the inspectionTray & sleeve inspection
Verify tray presentation, film seals, sleeve position, labels and traceability codes.
Explore the inspectionCap & closure inspection
Detect missing, high, skewed, wrong-colour or incomplete caps and closures.
Explore the inspectionLabel inspection
Check label presence, position, skew, artwork, barcodes and printed codes.
Explore the inspectionSeal inspection
Identify visible seal contamination, folds, gaps and incomplete closure conditions.
Explore the inspectionCase & pallet inspection
Verify cases, labels, codes, counts, closure and pallet build before despatch.
Explore the inspectionAutomatic reject integration
Track every inspection decision to a reliable, confirmed and contained rejection.
Explore the inspectionCan inspection
Inspect can bodies, lids, pull tabs, artwork, labels and printed codes on reflective packs.
Explore the inspectionBlister pack inspection
Check cavity contents, product position, foil, print, codes and visible pack presentation.
Explore the inspectionDate & lot-code inspection
Verify code presence, characters, print quality and the expected production recipe.
Explore the inspectionCode & barcode verification
Read and compare 1D, QR, Data Matrix and GS1 2D codes with the active job.
Explore the inspectionFill-level inspection
Detect visible high, low or missing fill conditions and combine them with closure checks.
Explore the inspection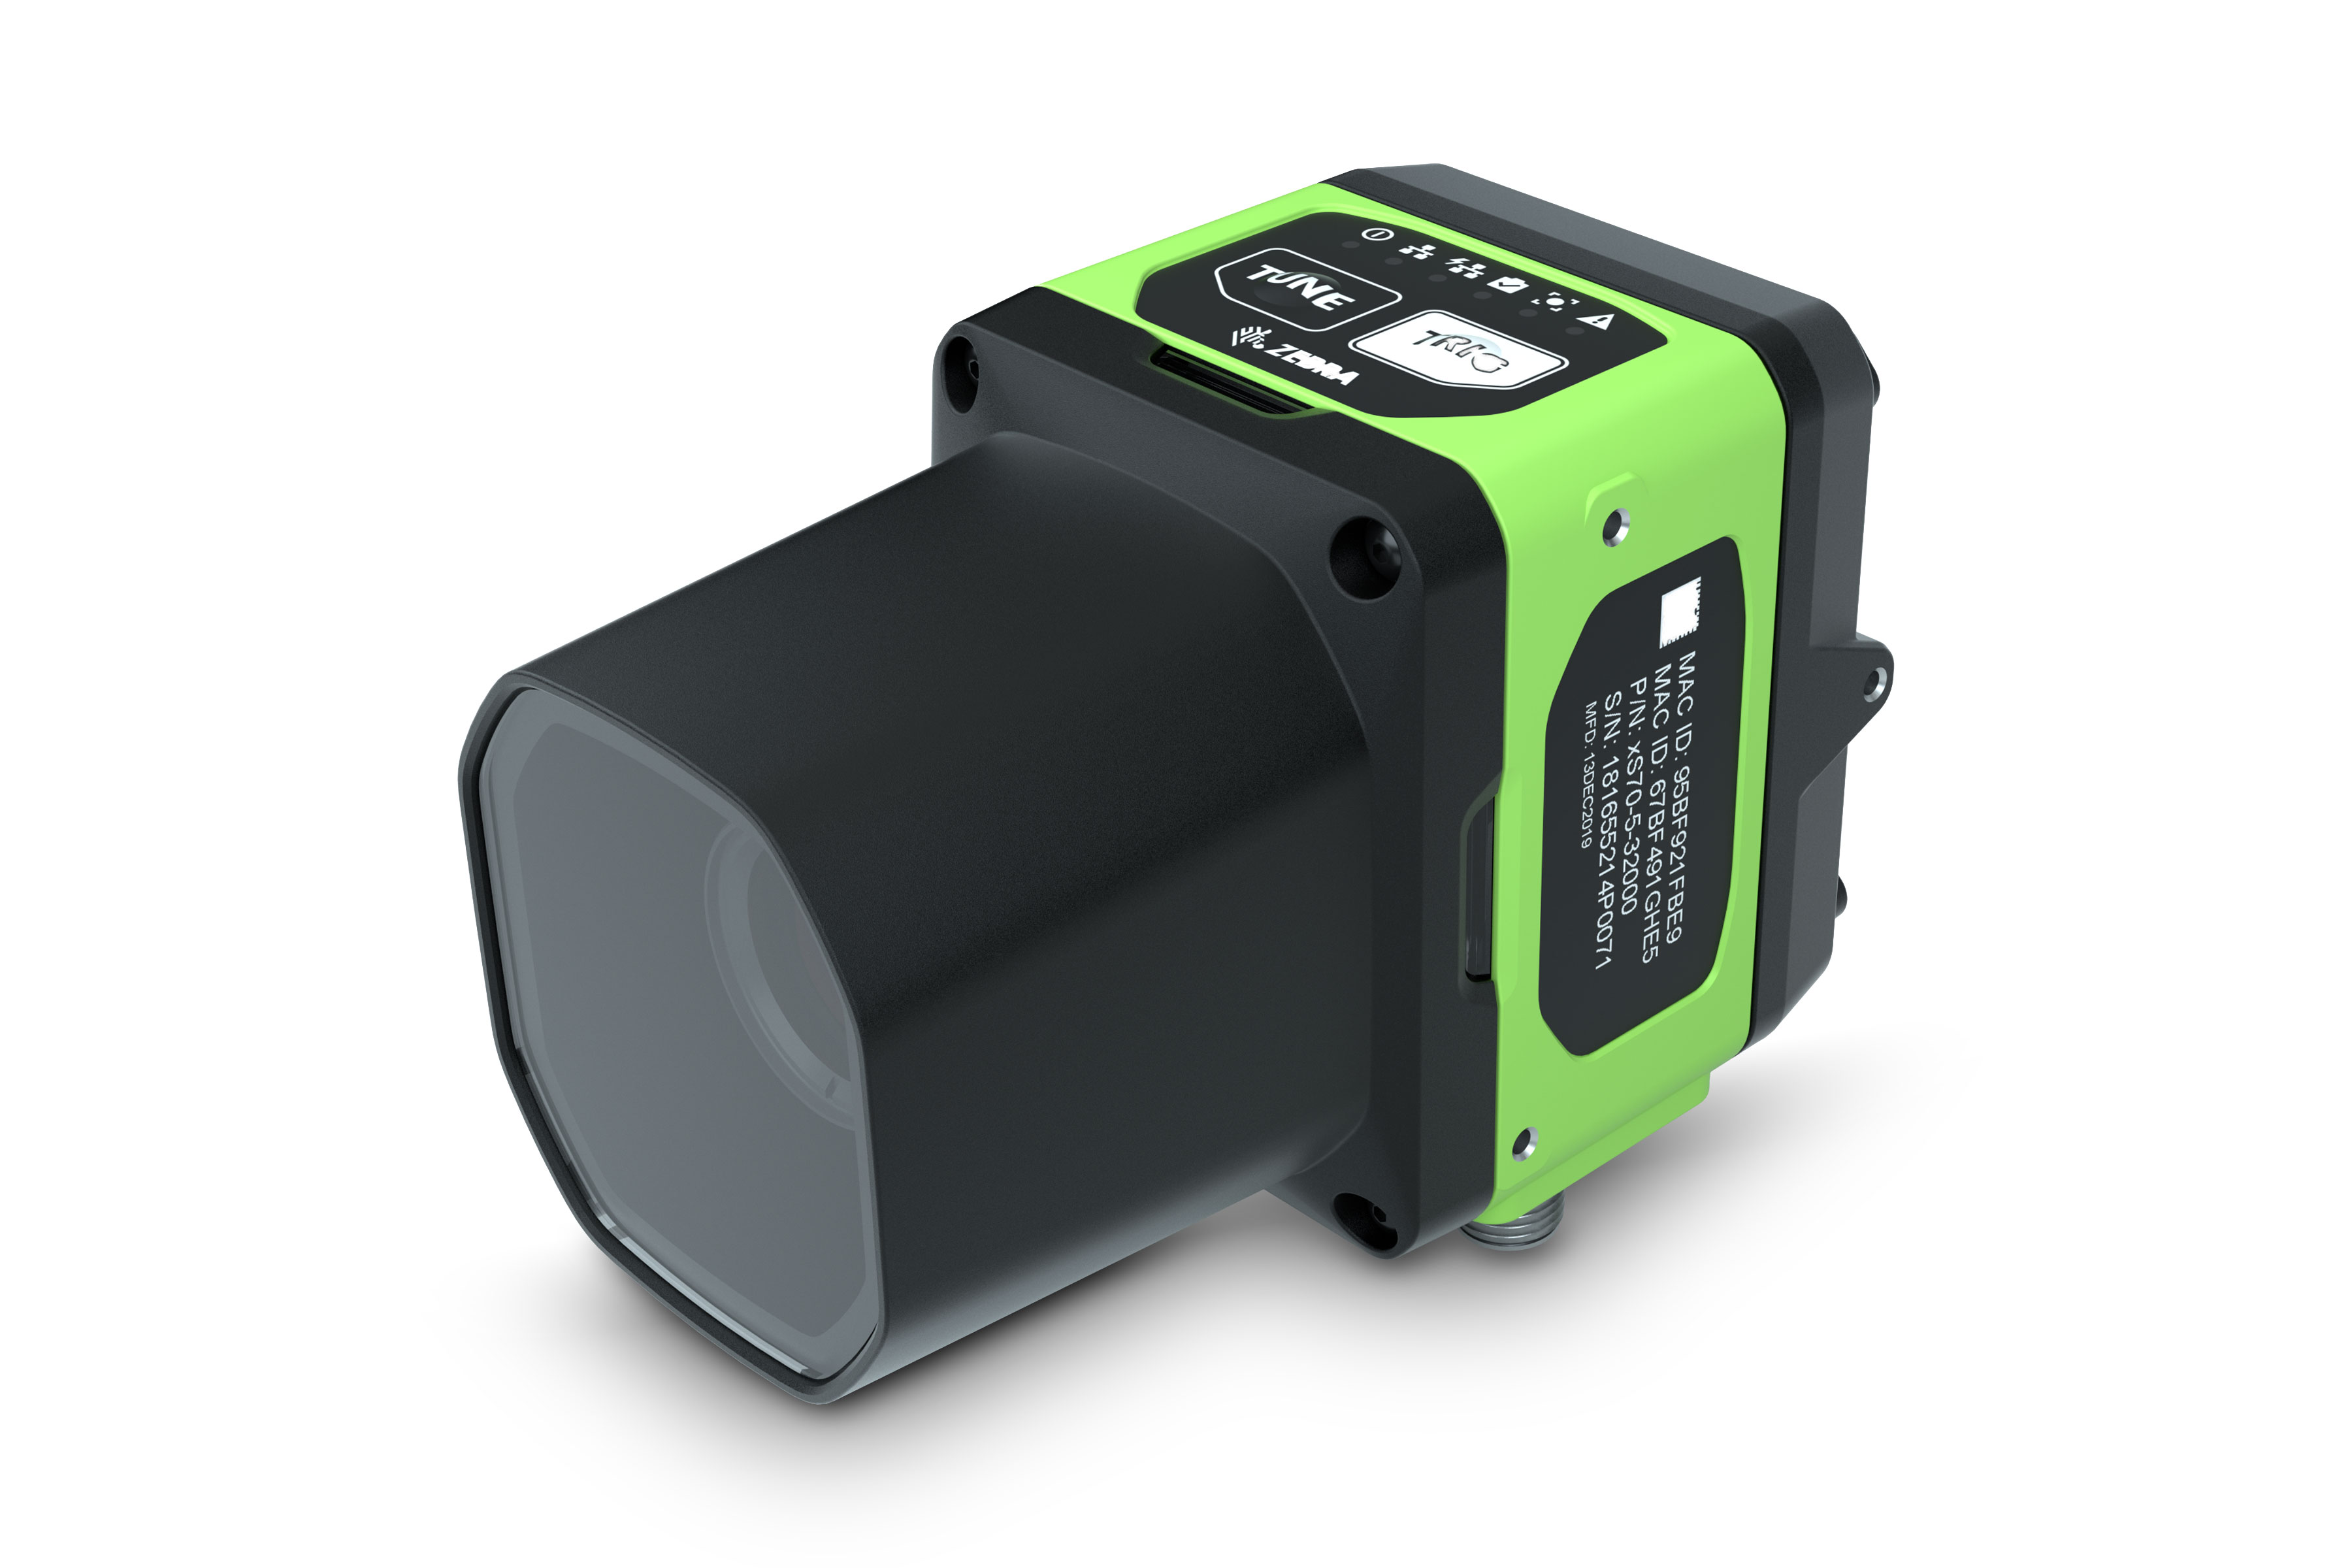
Not a generic camera package
Designed for your product, defect and production line
The inspection concept starts with what must be found and how the product is presented—not with a pre-selected camera.
- Good and defect samples
- Line speed and pack pitch
- Field of view and resolution
- Controlled industrial lighting
- Recipe and changeover design
- Conveyor and guarding review
- PLC and data interfaces
- Reject containment strategy
From image to action
One controlled inspection sequence
Product presentation, image capture, decision logic and physical rejection are engineered together for repeatable production use.
Present
Stabilise and space the pack so critical features remain visible.
Illuminate
Expose the feature with diffuse, back, dome or polarised lighting.
Decide
Apply calibrated measurements, matching, code and defect tools.
Contain
Track the result to confirmed rejection, alarm or controlled stop.
Inspection capabilities
Combine the checks your quality plan requires
A system can use several complementary tools in each view, while protecting inspection settings through controlled recipes and operator permissions.
Presence / absence
Confirm caps, labels, leaflets, inserts, seals and other required features.
Position / orientation
Measure placement, rotation, skew, height and relative alignment against tolerances.
OCR / OCV
Read or verify dates, lots, product text and selected printed characters.
Barcode / 2D code
Read 1D barcodes, QR and Data Matrix codes and compare content with the active job.
Colour / identity
Distinguish approved variants, colours, artwork and packaging components.
Dimensional checks
Measure visible edges, gaps, diameters, heights and profiles within calibrated views.
Surface defects
Identify visible damage, contamination, marks, chips, tears and presentation defects.
Seal appearance
Assess visible seal regions for contamination, folds, gaps and incomplete presentation.
Reject control
Track the decision to a guarded reject device, confirmation sensor and secure bin.
Automatic reject integration
Finding the defect is only half the system
We track every failed result to a suitable reject device and can add confirmation, bin-full monitoring, guarded containment and line-stop logic.
- Air blast, pusher, drop flap, diverter or retracting belt
- Encoder tracking and product association
- Reject confirmation and secure collection
- Consecutive-failure and fault handling
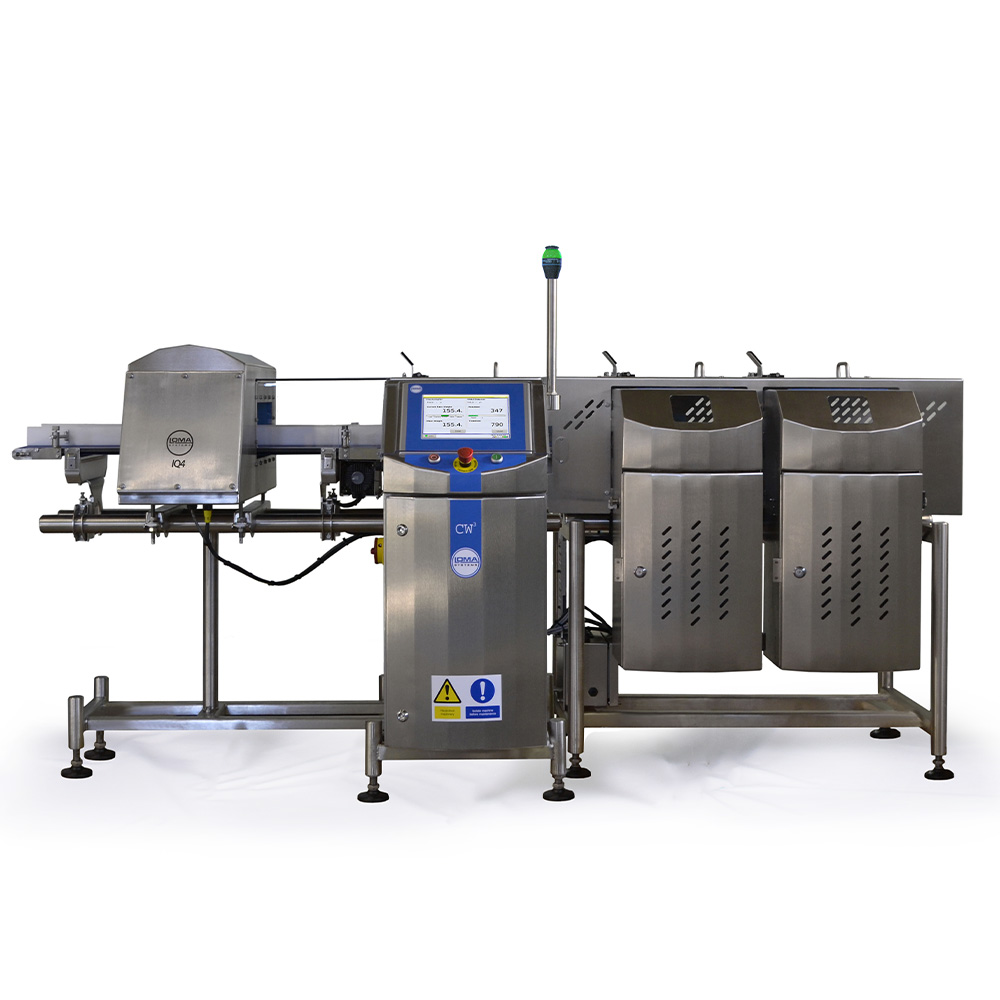
Manufacturer example: LOMA IQ4 metal detector and CW3 checkweigher with enclosed reject bins.
Connected production quality
Inspect where the feature is visible
Some checks belong before closure, others after labelling, sleeving or case packing. We map each requirement to the right point on the line.
- Pre-closure component presence
- Post-fill and post-cap inspection
- Label and code verification
- Seal appearance before it is hidden
- Case identity and closure checks
- Pallet pattern and label inspection
Solutions by industry
Inspection built around your production risks
Explore the packaging, quality and integration questions that matter in your sector.
Food packaging inspection
Labels, date codes, trays, pouches and visible seal presentation.
02 · BeverageBeverage packaging inspection
Bottles, fill indication, closures, labels, cases and pallets.
03 · PharmaceuticalPharmaceutical packaging
Identity, components, codes, controlled recipes and records.
04 · CosmeticsCosmetics packaging inspection
Premium finishes, pumps, caps, labels, artwork and batch codes.
05 · ChemicalChemical & household packs
Triggers, closures, hazard labels, codes, cartons and cases.
06 · Contract packingFlexible multi-SKU inspection
Controlled changeovers for customer artwork, formats and jobs.
Planning a project
Define feasibility and cost before purchase
Use our practical guides to prepare samples, line data, acceptance criteria and a comparable inspection brief.
Frequently asked questions
Planning a packaging inspection system
Practical answers to the first questions that shape camera, handling and reject design.
What types of packaging can a vision system inspect?
Systems can be configured for bottles, jars, pouches, cartons, trays, sleeves, caps, labels, cases and pallets. The camera, lighting and handling must be selected for the pack material, geometry, speed and defect.
Can inspection be added to an existing packaging line?
Yes, subject to available space, stable product presentation, guarding and controls access. A survey identifies the practical camera and reject positions and any conveyor modifications required.
Will machine vision keep up with our line speed?
Industrial cameras can inspect at production speed when exposure, resolution, trigger timing and processing are engineered together. Line speed, product pitch and smallest defect are confirmed during feasibility work.
Can the system reject failed products automatically?
Yes. The inspection result can operate a suitable air blast, pusher, drop flap, diverter or retracting belt, with encoder tracking, reject confirmation and secure collection where required.
Can inspection images and results be recorded?
Depending on the selected controls and storage design, systems can log counts, faults, recipes, result data and selected images. Retention, network access and data ownership are agreed during specification.
What information is needed for a quotation?
We need the pack formats, line speed, conveyor details, available space, environment, good samples and representative defects. A video of the running line and the required PLC or data interface are also helpful.
Read the inspection quotation and whole-project cost guide for scope exclusions, downtime assumptions and a clearly labelled comparison example.
Start with the product and defect
Define a practical inspection concept
Send us the pack formats, line speed, available space and the defects you need to catch. Samples and images are especially useful.
Can a camera inspect the seal on a pouch or tray?
A camera can assess a seal feature that remains visible and repeatable under the proposed lighting and pack presentation. That can include contamination, folds or visible gaps, while hidden channels and other integrity concerns may need a different test. The seal-inspection guide shows how to build an approved defect library, challenge normal film variation and connect optical findings with the product owner’s quality plan.
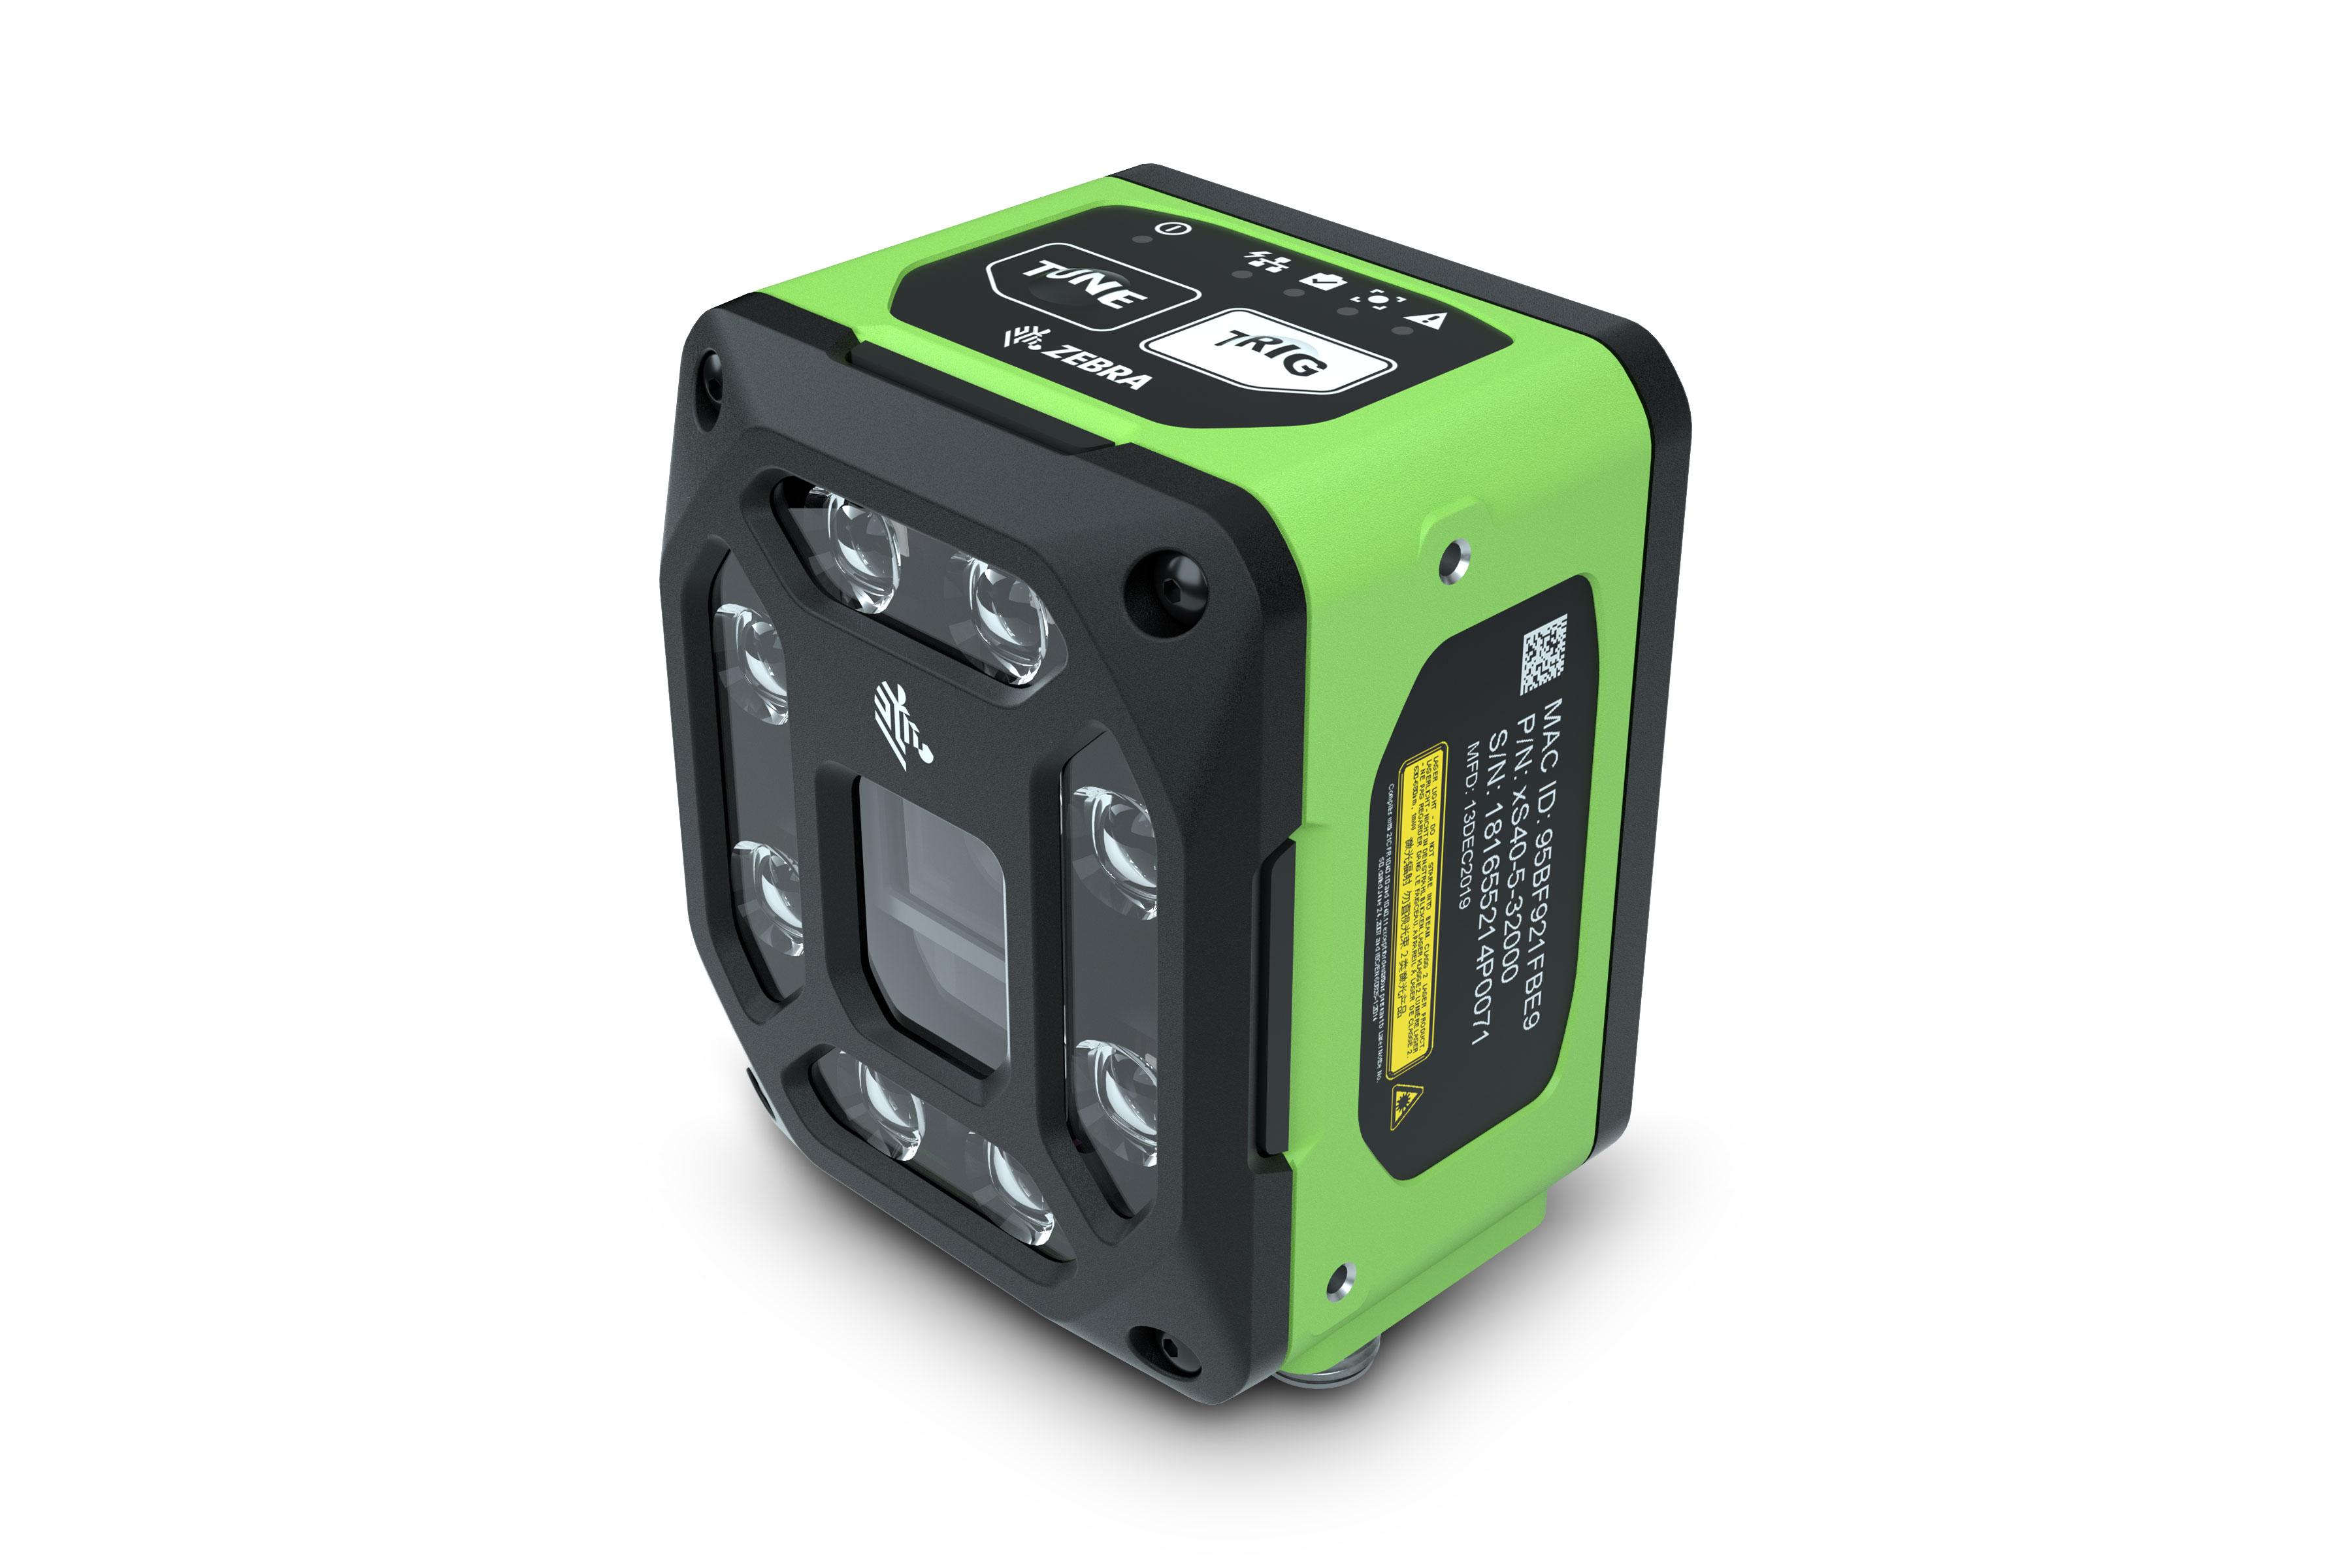
Manufacturer product photographs: Zebra machine vision camera from the VS70 product family; LOMA IQ4 metal detector and CW3 checkweigher combination system; Zebra fixed industrial scanner from the FS40 product family. Equipment examples; application-specific optics, controls and suitability are assessed separately. The LOMA example combines metal detection, checkweighing and enclosed reject bins.